Top 10 Spunlace Machine Types for Global Buyers
Spunlace Machine technology supports a rapidly expanding nonwoven industry, serving hygiene, medical, filtration, wipes, and personal-care applications. Global buyers now face more than a simple speed comparison. They must evaluate fiber compatibility, water-jet pressure, line width, energy use, wastewater treatment, and after-sales support.
Grand View Research estimated the global nonwoven fabrics market at approximately USD 53.5 billion in 2023. Its 2024–2030 analysis also indicates continued market expansion, driven by healthcare, hygiene products, and sustainable material demand. Smithers’ The Future of Nonwovens to 2029 identifies spunlace as an important growth area, especially for wipes and absorbent products. These reports suggest strong opportunity, but market growth alone does not guarantee a suitable machine choice. Details decide performance.
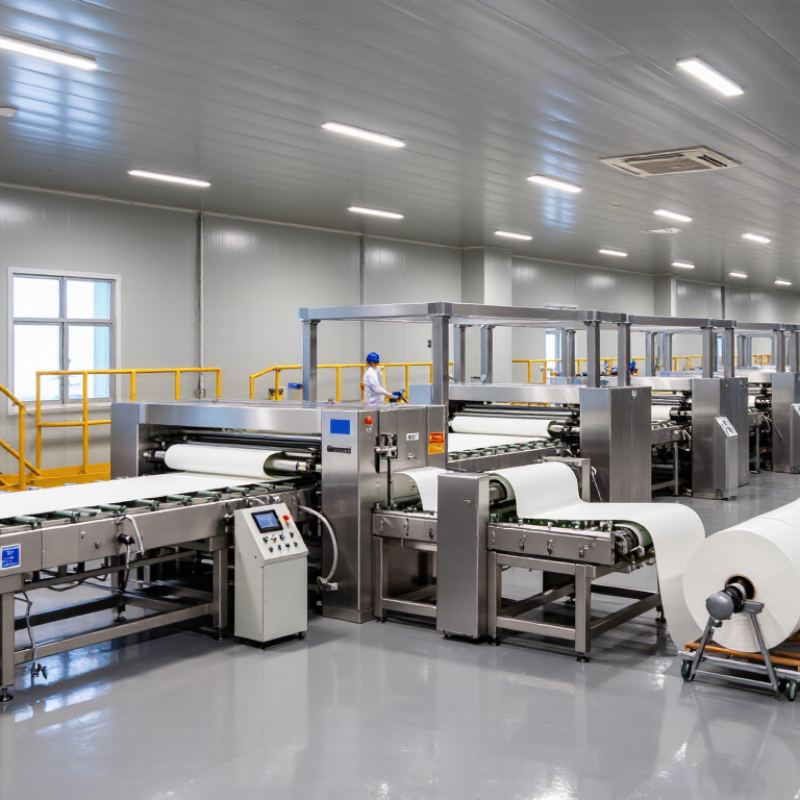
A modern Spunlace Machine may resemble a long steel corridor, with web-forming, hydroentangling, drying, winding, and control sections working continuously. A few nozzle-block differences can affect fabric strength, softness, and water consumption. Buyers should compare real production samples, not only brochures. No ranking is perfect. Machine categories overlap, and supplier claims require verification through trials, references, and documented operating data. This guide presents ten machine types for global buyers, considering production scale, fabric function, automation level, raw materials, and maintenance requirements. Some conclusions remain context-dependent. A compact line may outperform a larger system when factory space, labor, or wastewater capacity is limited. The practical question is not which machine looks most advanced. It is which machine delivers stable quality at the buyer’s actual operating conditions.
Spunlace Fundamentals: Hydroentanglement Pressures Commonly Reach 200 bar
Hydroentanglement is a deceptively simple process: fine water jets entangle fibers through a moving web. In many spunlace lines, operating pressure can reach 200 bar, depending on product requirements. That number describes capability, not a universal setting. Fiber type, web weight, nozzle design, and line speed all change the result. A heavier web may need stronger jet energy, while delicate fibers can suffer from excessive force. Small adjustments matter.
When comparing the top 10 spunlace machine types, buyers should examine pressure control as carefully as production speed. A useful system should provide stable pumps, accurate regulators, and accessible filtration. The water must remain clean. Blocked nozzles can create weak stripes, holes, or uneven softness. Operators often inspect jet strips and finished fabric after each pressure change. This practical check catches problems that a specification sheet may hide.
Higher pressure does not automatically produce better nonwoven fabric. It can improve bonding, but it may also reduce loft or damage fragile fibers. That trade-off deserves testing. Start with measured trials, record energy use, and compare tensile strength, absorbency, and surface feel. The best machine may offer control, not the highest pressure rating. Some setups still need refinement. That is normal.
Machine Comparison: 20–250 g/m² Basis Weights and 1–6 m Working Widths
Spunlace machine selection changes sharply between 20 and 250 g/m². For global buyers, the practical comparison covers ten configurations: single-card, double-card, parallel-lap, cross-lap, air-laid blending, flat-belt hydroentanglement, perforated-drum, multi-cylinder, compact pilot, and high-output wide-web lines. Light webs near 20–40 g/m² need careful web control and low-tension transfer. Heavy webs above 150 g/m² require stronger bonding energy and stable drainage. Working widths from 1 to 6 meters also affect frame rigidity, water circulation, and installation space.
In factory trials, I usually compare output at the same basis weight, not only the machine’s maximum speed. A 1-meter line may suit sampling and specialty materials. A 3-meter line often balances flexibility with production cost. Six-meter systems support large orders, but alignment errors become more visible across the web. Hydroentanglement pressure, nozzle arrangement, and drying capacity must match fiber type. Cotton, viscose, polyester, and blended webs can respond very differently. The specification sheet is useful, but it can hide difficult changeovers.
Tips: Test at three weights, such as 30, 100, and 200 g/m². Measure uniformity across the full width. Check water filtration, pump access, and cleaning time. Leave room for mistakes; first trials rarely reveal every operating weakness. A lower-speed machine with dependable control may outperform a faster system in daily production.
Top 10 Spunlace Machine Types for Global Buyers
Machine comparison by typical basis-weight capability and working width
The floating bars show representative basis-weight ranges from 20 to 250 g/m². The line indicates the typical maximum working width for each machine configuration. Actual specifications vary with fiber type, web-forming system, hydroentanglement pressure, drying capacity, and product requirements.
Global Buyer Metrics: Output, Water Recycling, Energy Use, and ISO 9073 Tests
Top 10 Spunlace Machine Types for Global Buyers
Global buyers should compare net saleable output, not nameplate speed. INDA’s Global Nonwoven Markets reports separate installed capacity from actual production, a critical distinction. A 2.5-meter line running at 120 meters per minute may deliver 180–300 kilograms per hour, depending on basis weight, fiber blend, and downtime. Buyers should request hourly production logs, web breaks, and changeover records. Output figures can look impressive. They can still mislead.
Water recycling deserves equal attention. EDANA sustainability guidance encourages reporting freshwater intake, discharge, and recirculation separately. A closed hydroentanglement loop may circulate many times more water than it consumes, so suppliers must disclose makeup water in cubic meters per tonne. Energy reports should identify drying, pumps, compressors, and wastewater treatment. A practical screening range is roughly 2–6 kilowatt-hours per kilogram, but boundary definitions vary. I would challenge any figure without a meter location and production recipe.
Quality verification should follow ISO 9073 methods. ISO 9073-1 measures mass per unit area, while ISO 9073-3 evaluates tensile strength and elongation. ISO 9073-6 addresses liquid absorption, and ISO 9073-10 measures lint and other loose-fiber release. Buyers should compare test conditioning, sample direction, and laboratory competence. Small details matter. A damp sample can distort results. Personally, I would require a witnessed trial using the intended fiber, basis weight, and line speed before selecting among the ten machine types.
Application Matching: Medical, Hygiene, Wipes, Filtration, and Geotextile Grades
Top 10 Spunlace Machine Types for Global Buyers
Application Matching: Medical, Hygiene, Wipes, Filtration, and Geotextile Grades
Choosing a spunlace machine starts with the finished material, not the equipment brochure. Medical grades need controlled web formation, fine water jets, low lint, and reliable contamination monitoring. The line should support stable basis weight across the full working width. Clean edges matter. Operators also need practical access for cleaning, inspection, and maintenance.
Hygiene and wipes require different performance targets. Wipe production often benefits from apertured drums, flexible web handling, and accurate moisture control. Cotton, viscose, polyester, and blended fibers can create different absorbency and strength profiles. Hygiene fabrics may require higher throughput and consistent softness. Wet strength testing is essential, especially when the material faces repeated handling. A faster line is not always better.
Filtration grades depend heavily on fiber selection, pore structure, and web uniformity. Spunlace machines with precise jet control can produce consistent surfaces, but filtration performance requires laboratory verification. Geotextile production usually demands heavier webs, stronger bonding, and careful cross-lap control. Edge stability becomes critical during installation. That gap matters. In my experience, buyers sometimes select a machine before defining tensile strength, absorbency, lint level, or operating width. This creates expensive adjustments later. A realistic trial should test raw materials, production speed, water pressure, drying capacity, and final-use performance.